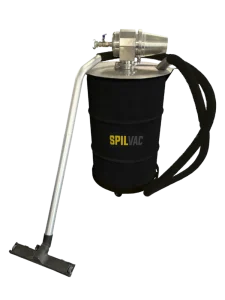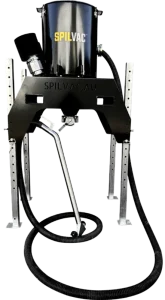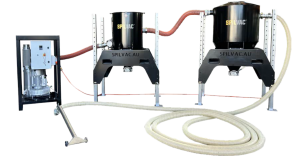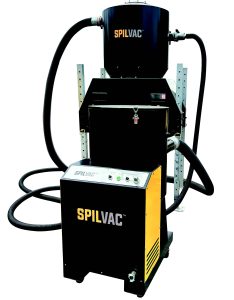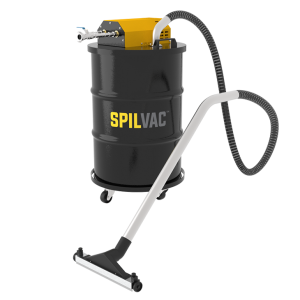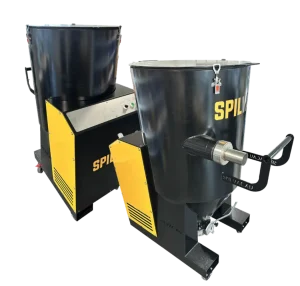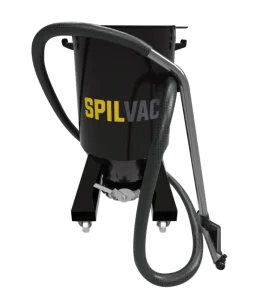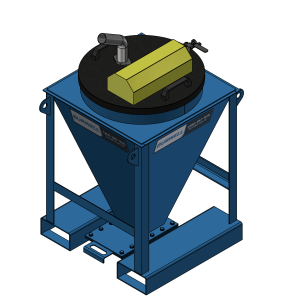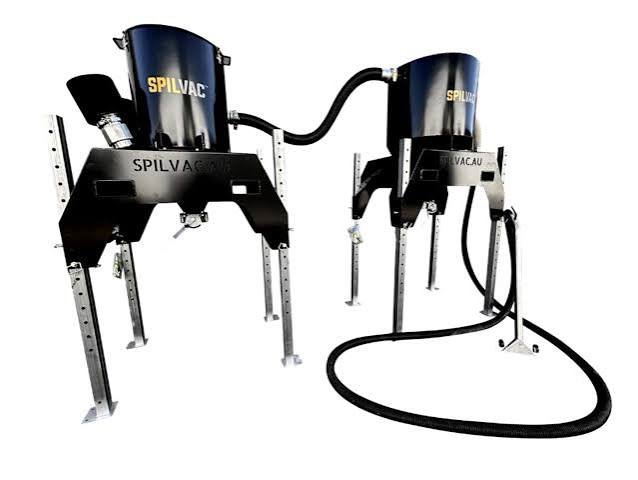
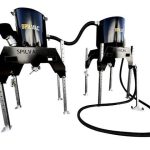
The Air Elevator System is a fully pneumatic vacuum system designed for both wet and dry product conveyance. It features a vacuum generator with a filter/dust separation hopper linked to a bulk hopper, ensuring efficient dust separation and increased filter life. This system is built with heavy construction quality, suitable for conveying large volumes of product over long distances.
The system is equipped with an automatic reverse pulse filter cleaning mechanism and comes with 20m of hose and a high wear floor tool. It is height adjustable and includes options for HEPA certified filters. The Air Elevator System is 100% Australian designed and manufactured, built to withstand heavy construction environments.
| Specification | Details |
|---|---|
| Practical Recovery Rate | 1-2 t/hr |
| Maximum Recommended Conveying Distance | 20m |
| Maximum Possible Conveying Distance | 30m |
| Compressed Air Supply Requirements | 100 CFM @ 80PSI |
| Air Flow Produced | 300 CFM |
| Maximum Vacuum | 609 Mbar / -18 InHGg |
| Hopper Capacity | 260 Litres |
| Noise Level | 70 dB |
| Weight | 600 kg |
| Method to Move Item | Fork lift Tyne slots |
| Options | Fully Stainless Steel construction – POA |
| Compressed Air Connection | 3/4″ Type A claw coupling |
| Compressed Air Supply Piping Diameter | 1 inch |
| Recommended Hose Diameter | 2 inch |
| Supplied Hose Type | High abrasive Antistatic |
| Vacuum Producer | Air powered Venturi |
| Filter Details | Spun Bond Polyester, 1 cartridge |
| Length | 1500mm |
| Width | 1100mm |
| Height | 1900-3000mm |
| Outlet | High Abrasive resistant manual butterfly valve |
| Floor Tools/Aspirator Details | Included |
| File Name | URL |
|---|---|
| AIR ELEVATOR SYSTEM.pdf | Download |
“Burwell has been a huge support to our operations at Kaefer, particularly in supplying high-quality air blast equipment, quality consumables, and abrasives that we rely on daily in the surface preparation industry. "

Kaefer
"I have used Burwell for four years now to supply all my blaster parts and consumables. During this time, I have found the staff and management team very customer focused and look for the best outcome for the client."

Vossloh Switch Systems Australia